Roundup: Chemical Industry Products to Watch - September 2026
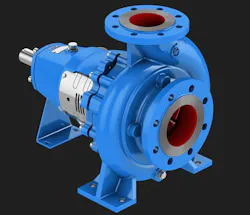
Chemical Process Pump Expands Hydraulic Coverage
Goulds Pumps introduced the ICi chemical process pump, expanding its isochemical pump portfolio with additional sizes and configurations for more precise pump selection.
The pump is available in 54 size varieties, 20 more than the existing IC range, with hydraulic capacity up to 1,600 m³/h. The expanded range is designed to provide broader hydraulic coverage for industrial processes, including chemical processing, oil and gas and water and wastewater applications.
The pump is available with closed or semi-open impeller designs. The semi-open configuration features a replaceable wear plate, adding another option for applications with different process requirements. According to the company, more precise pump sizing can help minimize wear, reduce maintenance requirements and extend equipment life.
The expanded range is intended to provide greater flexibility in matching pump performance to process conditions while supporting reliable operation across a broader range of industrial applications.
Flame Detector Adds Hazardous-Location Certification
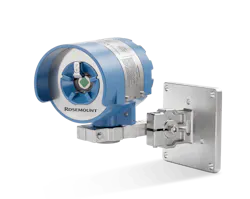
Emerson introduced a flameproof model of the Rosemount 965 flame detector, adding hazardous-location certification for applications requiring hydrocarbon flame detection.
The flame detector uses four infrared sensors to distinguish hydrocarbon fires from non-flame background radiation and help reduce nuisance alarms. Under specified conditions, it can detect hydrocarbon fires at distances up to 150 feet with response typically in less than five seconds. Five selectable sensitivity levels allow users to adjust detection performance for specific applications.
The detector is factory calibrated for life, which reportedly reduces recurring calibration requirements. Built-in infrared testing continuously verifies optics and electronics integrity, while HART connectivity and other output options support integration with existing communication infrastructure. Universal wiring is designed to simplify installation and IP66 and IP68 enclosure protection supports use in demanding environments.
The flame detector is intended for oil and gas facilities, chemical and petrochemical plants, storage tank farms and hazardous materials storage areas.
Articulating Video Borescope Simplifies Confined-Space Inspection
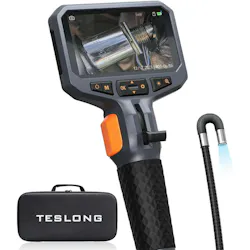
Paul N. Gardner Company introduced an articulating video borescope inspection camera with a two-way steering probe designed to inspect tight and complex spaces.
The borescope uses 180-degree two-way articulation to navigate narrow spaces with bends and turns, including tanks, pipes and mixing vessels. A flexible tip provides precise positioning in deep or confined areas, while a locking capability helps maintain the inspection position. The device displays video and images on a 4.5-in. IPS LCD color screen.
A high-brightness adjustable LED provides illumination in dark or confined spaces, while the display is designed for viewing in bright plant environments. The borescope also features a 5-ft. semirigid gooseneck cable that holds its shape and a centrally located joystick for one-handed operation.
A rear-mounted button enables photo and video capture for inspection documentation. The lightweight, compact design is intended to support extended use during inspections of equipment and confined process areas.
Dust Monitor Supports Hazardous-Area Emission Measurement
ABB introduced the PFM 20 Ex dust monitoring device, designed for continuous dust detection in hazardous and harsh industrial environments.
The dust monitor provides a certified detection range down to 7.5 mg/m³ and meets ATEX Zone 22 certification requirements. The device is designed to help operators monitor dust concentrations in applications where low-range measurement and equipment suitable for hazardous environments are required.
The monitor expands dust measurement capabilities for industrial emission monitoring and can be used alongside continuous emission monitoring, gas flow measurement and portable hydrocarbon detection technologies. The device is intended for industrial facilities requiring continuous measurement of particulate emissions in demanding operating environments.
The launch builds on measurement and analytical capabilities added through ABB's 2024 acquisition of Födisch Group, according to the company.
Oil-Free Diaphragm Vacuum Pump Offers Variable-Speed Operation
Pfeiffer Vacuum+Fab Solutions introduced the MVP 010-3 Neo, a three-stage oil-free diaphragm vacuum pump designed for applications operating in the 1-10 hPa pressure range.
The vacuum pump uses a frequency-controlled DC drive that allows rotational speed to be adjusted to the required vacuum level. According to the company, this reduces energy consumption and wear. The pump operates at noise levels below 50 dB(A) and includes an automatic boost mode to accelerate startup and evacuation.
An auto standby mode lowers rotational speed when full operation is not required, reducing noise, wear, temperature and power consumption. The pump also features an RS-485 interface for connection to turbomolecular vacuum pumps, external power supplies and control units. Accessory ports support options such as a gas-ballast valve for improved water vapor compatibility.
The compact pump is designed for integration into laboratory and research systems, including mass spectrometry, electron microscopy and X-ray applications.